Technology
Avoiding Costly Rework: A Data-Backed Framework for Selecting the Right Stainless Steel for CNC Machined Parts

Introduction
In the realm of accurate CNC machining, choosing an incorrect stainless steel alloy could be an insidious threatto your project budget and timeline. There are many instances when engineers face the unfortunate experience of having their projects fall preyto such oversimplified comparisons as “18/8 vs. 18/10” from online sources, only for actual failures to show up, as evidenced by pitting corrosion of medical devices or stress fractures of marine fasteners. Such failures inevitably leadto expensive consequences.
This article goes beyond the basics, offering you a powerful framework for making informed decisions about stainless steels. Utilizing information gathered from failure analyses and metallurgy, the article offers a methodology for matching alloy properties to environmental conditions and available technology. Ultimately, your focus will be on total cost of ownership rather than material cost.
What Are the Practical Ramifications of Selecting the Wrong Type of Stainless Steel?
Choosing an incorrect stainless steel grade begins a chain reaction of issues that may affect a company. While the immediate results include waste and expenses incurred for redoing the job, the long-term ramifications may be in the form of delays and damaged corporate image. Companies operating in highly regulated industries will also have to pay recall expenses and deal with negative audit findings.
1. Unseen Financial Burden Associated With Material Failures
An incorrect material choice leads to a series of hidden financial burdens. Apart from the obvious costs of redoing the project and the actual materials used, additional costs arise from rushed delivery, idle production lines, and warranty issues. To illustrate, a batch of parts delivered late after failing due to corrosion can rack up delivery costs more expensive than the cost of the parts themselves.
2. An Example of Material Selection in Conflict With the Environment
Imagine an actual case where 304 (18/8) stainless steel has been selected for a component of a medical device. Though appropriate in all aspects of its intended application, it has corroded due to pitting in response to the sterilization procedure using chloride-based chemicals in the hospital setting. This is not a manufacturing issue, but rather one of selecting an inappropriate material.
3. The Blind Spot During the Design Process
One cause of failure is that designers rely too much on the general materials table without checking with their manufacturing partners regarding any Design for Manufacturing (DFM) issues. This creates a scenario where a failure is expected but becomes an expensive problemto solve instead of a preventable one.
Moving Beyond 18/8 and 18/10: What Determines the Behavior of Core Materials?
These figures are merely simple shortcutsto expressing the chromium and nickel levels at roughly 18. 9% and 12. 8% respectively, with the overall performance regulated by how all the alloying elements in that particular batch of metal interact. An appreciation of the chemistry was crucial when judging how the material would resist corrosion and thereby remain strong.
l The Science Behind Corrosion Resistance: While it is true that chromium is inherently responsible for the formation of the passive oxide which defines stainless steel, the quantity of molybdenum within the alloy has a far greater effect on the alloy’s resistance to chloride-induced pitting corrosion. This is why 316 stainless steel (2-3% Mo) withstands this form of corrosion more readily than 304 stainless steel in chemical or marine environments.
l Relationship between machinability and performance: Not all stainless steel grades are equal in machining characteristics. Whereas free-machining types like the 303 grade improve chip-breakage and reduce tool wear, such stainless steels suffer from reduced corrosion resistance because of sulfur content. On the other hand, the 304 and 316 grades need advanced machining techniquesto counteract work hardening phenomena. However, this must be weighed in view of volume and tolerance considerations.
l Importance of standardization: As much as the ASME Y14.5 specification ensures uniformity in geometry tolerances across the globe, strict conformityto standards in material composition and heat treatment (ASTM, SAE) remains fundamental in assuring predictable material performance. Such standards are mandatory especially for parts used in aerospace and medical device assemblies.
Howto develop a material selection model in terms of application environment and loading conditions?
A rigorous selection process goes beyond a material datasheet and considers the whole picture. In essence, environment and mechanical loads become the key determinants in the selection process.
1. The Environmental Aggressiveness Matrix
The initial stage is to do a complete study of the environment. Humidity, salt spray, chemicals and temperature have to be studied carefully as regards material behavior. For internal use which is inexpensive and where humidity really is not a concern; 430 stainless steel seems to be the ideal material but if some humidity and chlorides are involved, the better choice would be 304 or 316.
2. Stress and Fatigue Analysis
Where heavy cyclic loads will act on the parts and/or in environments which tend to induce stress corrosion cracking, a choice between the austenitic (304/316) and martensitic (420) stainless steels is significant. Toughness and resistance to SCC of austenitic steels is considerably higher, therefore they are preferable for moving elements such as valve stems or fasteners.
3. The Total Cost of Ownership (TCO) Calculation
When considering a comparison between the four materials in a unit mass basis, remember that the ‘cheapest’ material of the moment can be orders of magnitude more expensive over time in service. Machining times, tool wear, scrap ratio, and possible rates of failure in the field are all relevant factors.
Are There Any Processes That Can Overcome Materials Deficiencies?
Whereas material characteristics are innate, there are advanced techniques in CNC machining that can be used to shape the performance of the finished product. An experienced CNC machining stainless steel manufacturer understands this concept and ensures maximum use of available material.
1. Eliminating the Effects of Work Hardening in Materials through Advanced Process
Work hardening is a problem in machining that affects stainless steels by causing damage and deformation in tools as well as poor accuracy of dimensions in machining. There are various approaches that can be employed to minimize this challenge, including use of sharp carbide tools with high-pressure cooling systems. This makes machining even tough types such as 304 possible.
2. Improving Resistance to Corrosion After Machining
Machining has a direct impact on the passive film. Passivation is vital as it helps restore and boost the effectiveness of the protective chromium oxide film, and gets rid of iron deposits that start corrosion processes. In case the component is used under particularly tough conditions, electropolishing will help improve the microfinish and corrosion resistance, effectively “rejuvenating” the surface after machining.
3. The Combined Power of Material and Process
Even the most experienced specialists cannot transform poor materials into high-quality parts, but they can bring out their best. As discussed in detail in a comprehensive analysis carried out by a recognized CNC machining stainless steel manufacturer, knowing the exact machinability rating of a particular type will help optimize parameters and achieve optimal dimensional stability and surface finish.
What Place Do Certifications and Quality Systems Hold in Safeguarding Material Integrity?
In precision engineering, there needs to be some system through which material integrity is guaranteed and not mere declarations. In this regard, certifications and quality systems offer the framework that assures us that we have the exact same material as prescribed and that the process undertaken in its production is right.
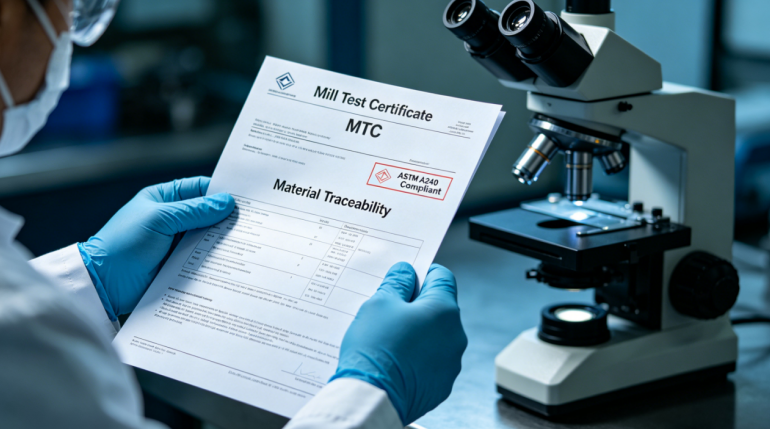
1. The Importance of Material Traceability
When it comes to crucial components, the first step towards safeguarding their integrity is through the Mill Test Certificates (MTCs). This certificate offers traceabilityto the point where the material was processed, and also assures the integrity of its chemistry and mechanical properties. It is imperative that the CNC machining services manufacturer offer this traceability.
2. Standardization and Control of the Process
The certifications mentioned above, namely ISO 9001 and AS9100, stipulate the need for systematic processes, including standard processes for incoming material inspections, first article inspections, and statistical process control (SPC). Such a discipline across the entire company will ensure that nothing will lead to an inabilityto perform as specified, such as improper heat treatment or contamination of materials during the handling process.
3. Risk Management in Highly Regulated Industries
The demands for process and supplier validation requirements in the medical industry standards, like the ISO 13485 or the aerospace industry AS9100D are very exacting. Dealing with a certified producer will enable you to establish a quality culture in your material decision making process and avoid any possible downsides of non-conformance.
How Can One Work with Their Manufacturing Partner To Make The Best Material Choice?
One of the best methods for avoiding unnecessary reworks is working with a manufacturing partner from the very start of the project, making material decision-making a joint engineering endeavor. By doing this, one will use their partner’s experience of what materials work best for production in reality.
1. The Benefits of Early Partnership: By consulting one’s CNC machining partner when they design a part, one will receive feedback on material selection due to DFM. The partners will be able to determine the manufacturability of different alloys concerning a particular geometry, recommend other grades that share similar characteristics yet have greater machinability, and identify possible sources of deformation.
2. Information Sharing for Well-Informed Decisions: When making well-informed recommendations, all the essential information must be shared with your partner in the form of a brief (part specifications, environmental considerations like temperature or chemical resistance, loading conditions, and industry-specific considerations like FDA or USP Class VI requirements). Your partner will then be able to analyze the out available materials and compare their costs.
3. Prototype Development & Testing Strategy: Apply prototyping not only as a tool for assessing form and fit, but also as a means of validating materials. Running a pilot with the selected grade can be used in a rapid test like the salt spray test, for example, to validate material performance prior to large-scale production.
Conclusion
Choosing the stainless steel for the machined part production is significant with process dependability, costs and time. Based on the criteria of the integration of scientific composition, environmental consideration and new methods of manufacturing, engineers will be able to prevent and control problems in advance. The most suitable material should meet not only functional requirement but also the total cost of the lifetime of the product.
FAQs
Q1: Is 304 (18/8) stainless steel suitable for parts that will be used outdoors in the coastal environment?
A: No, typically not advisable due to coastal chlorides leadingto pitting. However, a professional manufacturer of CNC machining services will help choose between other stainless steels such as 316 or other materials to balance durability with costs and avoid part failures.
Q2: What impact do materials have on lead time and cost of machined CNC parts?
A: Exotic, or less common, alloys would initially cost more because of the higher materials cost and increased processing time. That is, unless you use the wrong low-cost alloy then you’ll be forced to go back to the drawing board and remake the parts.
Q3: Have all the types of stainless steel been machined accurately?
A: Yes, with the benefit of stainless steel CNC machining, even all types of stainless steel have been machined accurately even distinguished between various types of steel contain various tooling parameters.
Q4: How do I know what the documents should be availableto check the grade of my parts?
A: They will provide Mill Test Certificates (MTC) for each batch of raw material they purchase. These are a requirement under ISO 9001 and seem to be a growing trend in the medical and aerospace industries.
Q5: When should I seek input from a manufacturing partner on selecting materials during my design process?
A: You should seek the consultation as soon as possible, preferably during the conceptual phase. This early consultation will help you receive useful DFM feedback in optimizing geometryto fit the material selected.
Author Bio
Author is an experienced precision manufacturing engineer working for LS Manufacturing, which provides engineering support for challenging parts development in aerospace, medical, and automotive industries. As a company that possesses IATF 16949 and AS9100D certification, the team offers state-of-the-art engineering services. Learn more about our experience by contacting us and having a free consultation and DFMA analysis of your project done by the professionals.


Running Facebook Ads without measuring performance can make it difficult to understand whether a campaign is achieving its goals. Businesses need to analyse campaign data to determine what is working, what needs adjustment and where advertising budget should be allocated.
Facebook Ads performance should not be judged by one metric alone. A campaign may receive many clicks but generate few enquiries, while another campaign may have fewer clicks but attract higher-quality leads.
Why Facebook Ads Measurement Matters
Tracking performance helps businesses understand:
- Whether ads are reaching the right audience
- Whether users are engaging with the content
- Whether campaigns are generating enquiries or sales
- Whether budget is being used effectively
- Which advertisements perform better
- Which audiences respond positively
Without measurement, businesses may continue spending on campaigns without knowing whether they are contributing to business goals.
1. Impressions
Impressions measure how many times an advertisement is displayed.
This metric helps businesses understand:
- How often ads appear
- How much visibility a campaign receives
- Whether the campaign is reaching enough users
A high number of impressions does not always mean a successful campaign. Businesses should review impressions together with clicks, conversions and cost metrics.
2. Reach
Reach refers to the number of unique people who see an advertisement.
Reach helps businesses understand:
- How many individuals saw the campaign
- Whether the campaign is expanding awareness
- Whether the audience size is appropriate
Reach is useful for awareness campaigns, but conversion-focused campaigns should also consider whether users take action after seeing the ad.
3. Click-Through Rate (CTR)
Click-through rate measures how many people clicked an advertisement compared with the number of times it was shown.
CTR can indicate:
- Whether the creative attracts attention
- Whether the message is relevant
- Whether the audience is interested in the offer
A low CTR may suggest that businesses should review:
- Ad visuals
- Copywriting
- Audience targeting
- Call-to-action
- Offer relevance
4. Cost Per Click (CPC)
Cost per click measures how much businesses pay, on average, for each click generated by an advertisement.
CPC helps businesses understand:
- Traffic acquisition cost
- Ad efficiency
- Audience competitiveness
- Creative performance
However, a low CPC does not automatically mean a campaign is successful. Businesses should also evaluate whether clicks lead to valuable actions.
5. Cost Per Result
Cost per result shows the average amount spent to achieve the campaign objective.
The result depends on the campaign goal, such as:
- Leads
- Purchases
- Website actions
- Messages
- Engagement
- App installs
Businesses should compare cost per result against business goals rather than looking at the number alone.
6. Cost Per Lead (CPL)
For lead generation campaigns, cost per lead is an important measurement.
CPL helps businesses understand:
- How much each enquiry costs
- Whether lead generation is sustainable
- Which campaigns attract enquiries
However, businesses should also review lead quality.
A campaign generating inexpensive leads may not perform well if the enquiries are not relevant.
7. Conversion Rate
Conversion rate measures how many users complete a desired action after clicking an advertisement.
Examples include:
- Filling out a form
- Making a purchase
- Booking an appointment
- Contacting a business
- Downloading a resource
Conversion rate helps businesses evaluate whether the landing page, offer and customer journey are working together.
8. Cost Per Acquisition (CPA)
Cost per acquisition measures the cost of obtaining a customer or completed action.
CPA is useful for businesses focused on:
- Sales
- Bookings
- Registrations
- Customer acquisition
Businesses should compare CPA against customer value to understand campaign profitability.
9. Return on Ad Spend (ROAS)
Return on ad spend measures revenue generated compared with advertising spend.
ROAS is commonly used by businesses that track direct revenue from advertisements.
However, ROAS may not apply to every campaign, especially:
- Awareness campaigns
- Branding campaigns
- Lead generation campaigns
- Long sales cycles
Businesses should choose metrics based on campaign objectives.
10. Frequency
Frequency measures how often the same user sees an advertisement.
High frequency may indicate:
- Audience fatigue
- Repeated exposure
- Need for creative refresh
Businesses should monitor frequency alongside engagement and conversion data.
11. Engagement Metrics
Engagement metrics show how users interact with advertisements.
These may include:
- Likes
- Comments
- Shares
- Saves
- Video views
- Reactions
Engagement can provide insights into audience interest and content relevance.
12. Video Performance Metrics
For video advertisements, businesses should review:
- Video views
- Average watch time
- Video completion rate
- Engagement
- Click actions
These metrics help identify whether videos capture and maintain audience attention.
13. Landing Page Performance
Facebook Ads performance is also affected by what happens after the click.
Businesses should review:
- Page loading speed
- Mobile experience
- Form completion rate
- Bounce rate
- Content relevance
- Call-to-action clarity
A strong advertisement may still underperform if the landing page does not meet user expectations.
14. Audience Performance
Businesses should analyse which audiences generate better results.
Review:
- Age groups
- Locations
- Interests
- Customer segments
- Retargeting audiences
- Lookalike audiences
Audience insights can help businesses refine future campaigns.
15. Ad Creative Performance
Different advertisements may perform differently even when targeting the same audience.
Businesses can compare:
- Images
- Videos
- Headlines
- Copy
- Offers
- Calls-to-action
Testing different creatives helps identify what resonates with the target audience.
How Often Should Businesses Review Facebook Ads?
The review frequency depends on campaign size, budget and objectives.
Businesses may review:
Daily
For:
- Spending issues
- Campaign errors
- Sudden performance changes
Weekly
For:
- Audience performance
- Creative performance
- Cost trends
- Lead quality
Monthly
For:
- Overall strategy
- Budget allocation
- Campaign goals
- Long-term performance
Regular reviews help businesses make informed adjustments.
Common Facebook Ads Reporting Mistakes
Looking Only at Clicks
Clicks do not always translate into business results.
Ignoring Lead Quality
A large number of leads may not help if they are not relevant.
Comparing Different Objectives
Awareness campaigns and conversion campaigns should not be measured using the same expectations.
Ignoring Customer Journey
Some customers need multiple interactions before taking action.
Making Decisions Too Quickly
Campaign data needs enough time before making major decisions.
Facebook Ads Metrics Businesses Should Track by Goal
Brand Awareness
Focus on:
- Reach
- Impressions
- Frequency
- Engagement
Lead Generation
Focus on:
- Cost per lead
- Lead quality
- Conversion rate
- Cost per result
E-commerce Sales
Focus on:
- Purchases
- CPA
- ROAS
- Conversion rate
- Revenue
Website Traffic
Focus on:
- Click-through rate
- CPC
- Landing page behaviour
- Website actions
Measuring Facebook Ads performance requires looking beyond basic engagement numbers. Businesses should analyse a combination of delivery, engagement and conversion metrics to understand whether campaigns are supporting business goals.
Metrics such as CTR, CPC, CPA, ROAS, conversion rate and cost per result provide useful insights, but they should always be evaluated alongside campaign objectives and customer quality.
This article is for general information only and should not replace advice from a qualified digital marketing professional.


An egg roll machine sounds like a straightforward search. It is not. The phrase can refer to a domestic cooker, a machine for a fried savoury wrapper, or equipment that bakes a fine batter sheet and rolls it while hot into a crisp sweet product. The names overlap, while the ingredients, heat path, forming action and output units do not.
That is why an output figure should be read last rather than first. This guide starts with the finished article and follows the main production routes that sit behind the search term. It explains plate baking, hot rolling, parallel baking lanes and core injection, then shows which questions need to be answered before a buyer turns an egg roll machine inquiry into a comparable quotation.
What an egg roll machine is supposed to make
UDTECH separates the names by cooking route. Its sweet roll equipment bakes a fine batter sheet and rolls it while the sheet is still hot and flexible. The same page distinguishes that product from a savoury wrapper that is formed cold around a filling and fried later. The finished product, rather than the phrase in a search box, tells the buyer which route belongs in the conversation.
Ask for a photograph, finished length, diameter and one-piece weight before discussing a machine family. Those details identify whether the project is a crisp hollow roll, a filled wafer roll, a flat baked piece or a fried wrapper. They also reveal whether the product needs rolling after baking or needs a completely different forming method.
Baked wafer rolls: deposit, bake and roll while hot
For a sweet baked egg roll, batter is deposited onto a heated plate, baked into a thin sheet, then folded and rolled before it loses flexibility. The result is a hollow crisp roll whose wall thickness depends on the deposit and plate gap. This route joins shaping and heat closely: the forming action happens while the baked sheet is still capable of becoming a tube.
Where it stops: this process does not make a fried savoury roll. A cold wrapper with filling is formed before its cook step, so it needs a different product path. Choosing a hot-roll machine because the final foods share a name leads to the wrong process before output has even been considered.
Baking plate route: a format-driven choice
UDTECH lists small rotary configurations in daily-capacity bands, including 125–175 kg for one hand-style route and 250–350 kg for another. Those are model-specific daily figures, not a generic promise for every type of egg roll. Their value is that they keep the product, plate process and stated unit in the same decision.
This rotary mechanism repeats the plate-and-roll cycle through multiple mould positions. That can suit a project where the finished roll and its dimensions fit the plate arrangement. It also means the buyer should check colour, crispness, seam condition and roll geometry on the actual sample rather than assuming a similar-looking tube will behave the same way.
Where it stops: a larger mould count is not a licence to change the product format without review. A different diameter, wall thickness or surface layer can alter deposit behaviour, bake response and rolling performance. The piece must still leave the plate in a condition that can be rolled cleanly.
Parallel baking lanes and hot rolling: a continuous route
UDTECH’s gas-fired roll lines bake the batter on parallel lanes, then core and roll-form the product in line. Its published page gives the continuous models a production band of 600–900 kg per 8-hour shift. More than the number matters here: the baked sheet passes into the next forming operation as part of one continuous process rather than stopping for a separate manual roll step.
Where it stops: a continuous line cannot be selected from daily mass alone. Plant teams still have to establish the fuel, exhaust, air, cooling and packing boundary for the approved roll. A capacity number does not show whether a product with a chosen filling, coating or fragile shell can make that whole handoff without damage.
Core injection changes the product brief
UDTECH identifies core injection as a line operation for its continuous roll models: filling enters the tube before the roll cools and hardens. That makes the filling a product variable, not a decorative detail added after the machine is selected. Its viscosity, intended fill condition and the shell’s tolerance all belong in the trial brief.
Where it stops: an injection feature cannot repair a shell that is weak, badly rolled or incompatible with the filling. The product must first be able to leave the baking and rolling stages as a stable tube. Only then can a buyer judge the downstream effect of a filled product on cooling and packing.
Why release begins before the release point
According to the American Society of Baking’s wafer-process reference, fat supports release and emulsifiers help steam escape during baking. Its discussion concerns wafer production, but the lesson is directly relevant to a baked egg-roll sheet: release is shaped by the batter and bake before a mechanism touches the finished piece. Plate condition, deposit, heat and time need to be reviewed as a connected set during a product trial.
That is why a release issue should not be reduced to a request for a harder scraper or a faster roll station. If the sheet has not reached the required condition, changing the final contact may only move the damage downstream. The better test asks whether the approved sample releases and rolls with the required wall condition and appearance.
Output units should never be silently converted
The UDTECH category page uses several legitimate capacity bases, including kilograms per day, pieces per hour and kilograms per shift. It also lists 380 V three-phase supply and compressed air above 0.6 MPa for the category. Each entry answers a different question. Capacity needs a product and time basis; electrical supply and air pressure describe site readiness.
A buyer should not convert between pieces and mass using an assumed roll weight. A filled tube, a hollow tube and a roll with a different wall thickness can all change the result. Keep the supplier’s original unit visible until the finished piece and operating basis are confirmed in the product brief.
How a supplier fits into the product discussion
The udmachine.com product description makes the route visible before it asks a buyer to compare capacity. Start there. A broad food name offers less help than a clear account of what is baked, rolled and passed downstream.
UDTECH is useful in two separate parts of the selection process. First, its product route makes the category boundary visible: a baked roll and a fried wrapper are not alternatives within one machine. Second, the listed rotary and continuous routes show why output numbers must stay attached to their process and utility requirements.
That does not make a published specification an acceptance result. The buyer still needs to supply the finished sample and define what counts as an acceptable roll. Product geometry, texture, filling condition and the point where the product moves to cooling or packing should be agreed before a selected configuration is treated as final.
Questions to settle before asking for a quotation
Use the udmachine.com route as a prompt for the first conversation, then test every claim against the buyer’s own sample. A product photograph is useful. Its production path is the deciding evidence.
Send a photograph of the finished product with its dimensions, intended piece weight and whether the tube is hollow or filled. State whether the sheet must be baked and rolled hot or whether the product is a cold wrapper that will be fried. Then give the target output on one explicit time basis, plus the available power, air, fuel, exhaust route and downstream packing plan.
With that information, a buyer can compare UDTECH egg roll equipment with another suitable route without confusing a product name for a manufacturing answer. An egg roll machine is selected when the finished piece, its cooking path and its output unit describe the same project.

Core Insights
- CoaXPress technology delivers the high bandwidth and low latency required for demanding, real-time industrial inspections.
- Single-cable solutions simplify complex system installations and reduce maintenance needs on the factory floor.
- High-speed manufacturing environments benefit from the extreme reliability and precision offered by advanced camera standards.
- Proper data management ensures that production lines maintain speed without sacrificing inspection accuracy.
The Big Picture
Have you ever stopped to wonder how modern factories maintain such incredible precision while operating at blistering speeds? It is a constant race against time. Every component, from a tiny microchip to a larger automotive part, must be inspected instantly. If the imaging system lags, the production line grinds to a halt. This is where the right hardware becomes your best friend. Choosing a CXP Camera is often the turning point for engineers looking to balance speed with high-quality image capture. When you rely on high-speed imaging, you need a system that doesn’t just keep up, but sets the pace.
Why Is CoaXPress The Standard For High-Speed Imaging?
When dealing with high-speed applications, standard interfaces often fall short. They simply cannot push enough data through the pipeline without creating a bottleneck. CoaXPress emerged as the answer to this common frustration. It provides a massive pipe for data to flow through, ensuring that high-resolution images reach the processing unit without delay.
Think of it like moving from a narrow country lane to a multi-lane motorway. You can move much more traffic, in this case, image data, at significantly higher speeds. This capability allows for complex inspection tasks to happen in real-time. By keeping latency low, you ensure that any defect is identified the moment it appears. It isn’t just about the raw speed, though. It is about the consistency of that data stream. When your production process relies on millisecond timing, having a reliable flow of information is critical. You want a system that remains steady, hour after hour, without dropping a single frame.
How Does A Simplified Cabling Setup Help Your Production Floor?
Anyone who has worked on a complex industrial machine knows that cable management can become a nightmare. You have power cables, data cables, and trigger cables all fighting for space. This clutter is not just messy; it is a liability. Every extra cable is a potential point of failure. This is where a CXP Camera shines by simplifying the architecture.
Because CoaXPress combines data transfer, communication, and power into a single cable, you immediately reduce the physical footprint of your setup. You aren’t just saving time during the initial installation; you are also making life easier for your maintenance team. If something does go wrong, you are troubleshooting one line instead of a tangled web of connections. It is a clean, efficient way to handle what used to be a messy problem. By streamlining your connections, you create a more robust setup that is easier to manage and less prone to those frustrating, hard-to-trace connection issues that plague so many assembly lines.
How Do Modern CXP Camera Products Withstand Industrial Rigours?
Reliability is non-negotiable in an industrial setting. Factories are not sterile laboratories. They can be dusty, vibrate intensely, and often involve fluctuating temperatures. If your hardware is fragile, your inspection process will fail when you need it most. This is why engineers look carefully at the build quality of their imaging equipment.
Modern CXP Camera products are engineered to thrive in these demanding conditions. They are built to endure the vibrations of heavy machinery and the heat of continuous operation. When you select high-quality imaging hardware, you are investing in longevity. You want a sensor and an interface that are as tough as the environment they operate in. It is about peace of mind, really. You set the system up, and you can trust that it will keep working through the shifts. This stability reduces downtime, which keeps your output consistent and your costs predictable. It is a classic case of getting what you pay for; investing in durable, purpose-built technology saves you from constant replacements and emergency stops.
What Makes The CXP Camera Essential For High-Speed Inspection Tasks?
At the end of the day, inspection is about catching what the human eye misses. Whether you are checking for microscopic surface scratches or verifying the presence of critical components, the CXP Camera provides the necessary clarity and speed. It isn’t just a sensor; it is a high-performance tool that bridges the gap between raw motion and actionable data.
| Feature | Benefit |
|---|---|
| High Data Bandwidth | Supports massive data flow for high-resolution images without bottlenecks. |
| Single Cable Solution | Combines data, power, and control to simplify cabling and reduce failure points. |
| Low Latency | Enables real-time processing and immediate defect identification. |
| Industrial Durability | Withstands harsh environments, including vibrations, heat, and dust. |
The ability to process such large volumes of image data in real-time allows for more complex algorithms to run on the back end. You aren’t just taking pictures; you are performing sophisticated analysis on the fly. This level of detail ensures that your quality control is tight, preventing bad parts from slipping through to the next stage. When your imaging system is this efficient, your entire production workflow becomes more fluid. You spend less time worrying about your cameras and more time focusing on what really matters: the quality of your products and the efficiency of your line.
Ready to Elevate Your Inspection?
High-speed industrial imaging requires a delicate balance of speed, reliability, and ease of use. By leveraging CoaXPress technology, manufacturers can ensure that their inspection lines remain efficient and accurate, even under the most demanding conditions. Whether it is simplifying your cabling to reduce failure points or ensuring your hardware can handle the heat of the factory floor, the right technology makes a massive difference. If you are ready to upgrade your inspection capabilities, reach out to the experts at Voltrium Systems for solutions tailored to your specific needs.

Portable Laser Welding Machine Maintenance Guide

Restoring Strength and Safety: Comprehensive Alzheimer’s & Post-Hospital Elderly Care in Phoenix

The Enduring Appeal of Batman: Why Every Generation Finds Its Own Dark Knight

Top Digital Marketing Agencies for Multi-Channel Campaign Success

How Technology Is Changing the Way We Learn to Drive

Keeping Dogs Clean After Muddy Outdoor Adventures

The 15 Highest-Paid Rugby Players in the World
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon

How to Ensure Your Home is Valued Correctly for a Quick Sale

What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement

Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats
Nancy Hallam: The Inspiring Life, Career, and Success Story Behind Ian Wright’s Wife
The 15 Highest-Paid Rugby Players in the World
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon
How to Ensure Your Home is Valued Correctly for a Quick Sale
What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement
Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats
Nancy Hallam: The Inspiring Life, Career, and Success Story Behind Ian Wright’s Wife
-
 Sports4 months ago
The 15 Highest-Paid Rugby Players in the World
-
Celebrity10 months ago
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon
-
 Real Estate8 months ago
How to Ensure Your Home is Valued Correctly for a Quick Sale
-
 Technology4 months ago
What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement
-
 Celebrity3 months ago
Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats
-
Celebrity10 months ago
Nancy Hallam: The Inspiring Life, Career, and Success Story Behind Ian Wright’s Wife
-
 Health8 months ago
Enclomimed 25 (Enclomiphene) – Effective PCT Protocol
-
 Celebrity10 months ago
Who Is Maisie Mae Roffey? The Private Life, Family Story, and Quiet Success of Julie Walters’ Daughter