Tech
Laser Welding Stainless Steel for Sheet Metal and Fabrication

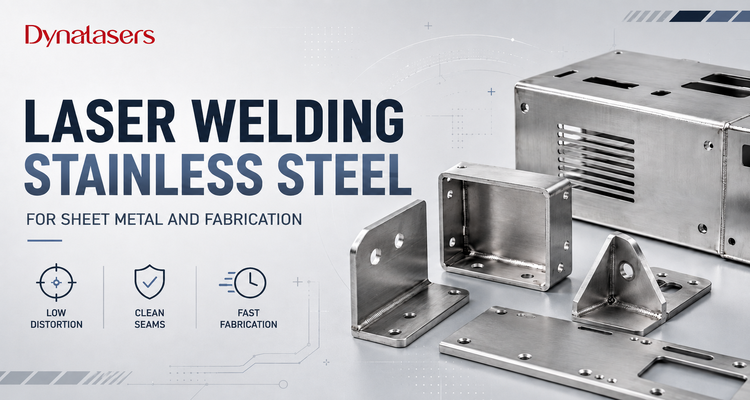
Laser welding stainless steel works particularly well on sheet-metal parts where distortion, seam appearance, and finishing time matter. Dynalasers handheld systems cover lightweight repair through higher-power fabrication, with air-cooled models from 700W to 1800W and published stainless-steel melting depths from about 2.5 mm to 7 mm depending on model.
The process is fast and concentrated, but good stainless welds still depend on fit-up, cleanliness, shielding gas, travel speed, focus, and penetration. A bright-looking bead alone does not prove a sound joint.
Can Stainless Steel Be Laser Welded?
Yes. Austenitic stainless grades such as 304 are well suited to fiber laser welding, and research has demonstrated strong joints with low angular distortion when power, speed, beam position, and joint preparation are properly controlled. One study on 6 mm SS304 achieved full penetration with angular distortion below 0.8° and joint efficiency around 83–85%.
For handheld fabrication, the main attraction is concentrated heat. A narrow heat source can reduce the amount of surrounding sheet that expands and contracts during welding. That is valuable on cabinets, kitchen equipment, doors, housings, covers, and other finished stainless products where distortion often creates more work after welding.
Still, laser welding steel does not remove the need for process control. Stainless sheet can burn through when energy is too high, while excessive speed or poor fit-up can leave shallow fusion.
Laser Welding Stainless Steel vs TIG and MIG
| Method | Heat Input | Speed | Gap Tolerance | Typical Finish Work | Best Fit |
| Laser welding stainless steel | Concentrated | High on suitable joints | Lower | Often limited when parameters are stable | Sheet metal, visible seams, repeat fabrication |
| TIG welding | Controlled but broader | Slower | Moderate | Usually low with skilled welding | Precision manual work, repair, cosmetic welds |
| MIG welding | Higher overall heat | Moderate to high | Better | More spatter or dressing may be required | General fabrication, larger gaps, heavier work |
Handheld laser welding can reduce post-weld work because of its concentrated heat input and narrow seam, and AWS notes that the process has attracted manufacturers partly because of higher throughput and reduced finishing requirements.
That does not automatically make it better than TIG or MIG. If a fabrication line has inconsistent gaps, dirty parts, thick structural joints, or an established qualified arc-welding procedure, conventional welding may still be easier to control.
What Actually Controls a Stainless Steel Laser Weld?
Power gets the most attention, but it is only one variable.
A stable weld comes from the relationship between laser power, travel speed, focus position, wobble width, joint geometry, wire feed, and material thickness. Research on stainless fiber laser welding shows that power, speed, beam spot size, and edge preparation all influence penetration, bead shape, and distortion.
This matters when reading machine specifications. Dynalasers, for example, publishes the following single-sided melting depths for stainless steel:
| Dynalasers Model | Power | Published Stainless Steel Melting Depth |
| S30 | 700W | 2.5 mm |
| M30 | 800W | 3.0 mm |
| M50 / D50 | 1200W | 5.0 mm |
| D60 | 1500W | 6.0 mm |
| M70 / D70 | 1800W | 7.0 mm |
These are useful capability references, but they should not be treated as guaranteed production thicknesses. Actual joint penetration changes with fit-up, joint type, travel speed, focus, material condition, and acceptance requirements.
For critical work, check the cross-section instead of judging only the top surface.
Fit-Up Matters More Than Many First-Time Users Expect
A sheet metal laser welder works with a concentrated beam, so inconsistent gaps become obvious quickly.
A tight butt joint may weld autogenously without filler. Once the gap increases, wobble can help widen the effective processing area, but it does not create missing metal. Filler wire may then be needed to bridge the joint and build the required bead.
This is one reason laser welding often performs particularly well in shops with repeatable laser-cut or CNC-formed components. If the parts arrive with predictable edges and stable fixturing, the welding process becomes easier to repeat.
Oil, fingerprints, cutting residue, oxide, and moisture should also be removed from the joint area. Contamination can affect the weld pool and leave porosity or surface discoloration.
Shielding Gas Is Not Simply “Argon or Nitrogen”
Argon is a common practical starting point for stainless welding, but shielding gas should not be treated as a universal setting.
Research has shown that nitrogen and argon can affect stainless weld metallurgy differently. In duplex stainless steel, for example, nitrogen shielding can increase austenite content and improve toughness compared with argon under specific welding conditions. Other studies on austenitic stainless steels have also found that nitrogen uptake changes with the shielding atmosphere.
So the right question is not:
“Is nitrogen better than argon?”
It is:
“What gas is appropriate for this stainless grade, joint, and required weld properties?”
For everyday 304/316 fabrication, start from the equipment and procedure recommendation, then confirm appearance and weld quality on samples. Duplex, high-nitrogen stainless, or corrosion-critical parts deserve more specific procedure development.
Heat Tint Is Useful Information, but Not a Weld Test
Stainless laser welding often produces a much narrower heat-tinted area than conventional welding because less surrounding material is heated.
That is good for appearance, but color alone should not be used as the quality standard. A clean silver bead can still have insufficient penetration, while a mechanically sound weld may show surface oxidation if gas coverage is poor.
Full-penetration joints also deserve attention on the reverse side. If the backside is exposed to air while hot, heavy oxidation can develop even when the front looks acceptable.
For decorative sheet-metal work, appearance may be the main concern. For food equipment, chemical service, or corrosion-sensitive assemblies, surface condition and post-weld treatment can matter much more.
Where Laser Welding Stainless Steel Works Best
Laser welding sheet metal is especially useful when the finished part needs to stay straight and presentable.
Typical work includes stainless cabinets, electrical enclosures, kitchen equipment, counters, sinks, doors, elevator components, machinery covers, furniture, tanks, brackets, and fabricated housings.
A stainless steel spot laser welding machine can also be useful where continuous seams are not required. Spot or pulse modes allow localized joining, tacking, repair, and control of heat input on smaller areas.
For high-volume automated assemblies, fixed laser cells may still be more appropriate. Handheld systems make more sense when the shop handles different sizes, short production runs, repair, and frequent changeovers.
Dynalasers M Series for Everyday Stainless Fabrication
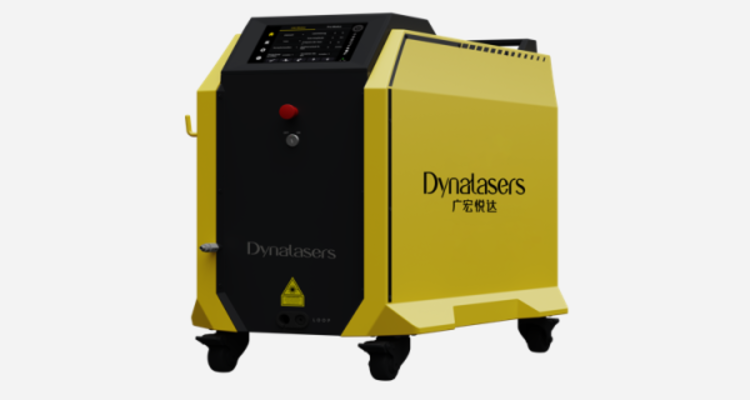
The M Series covers M30, M50, and M70 at approximately 800W, 1200W, and 1800W. All use air cooling and combine welding with cleaning and light cutting functions. Dynalasers lists stainless melting depths of approximately 3 mm, 5 mm, and 7 mm across those three power levels.
That range makes the M Series practical for shops moving between cabinets, frames, sheet assemblies, repair parts, and general stainless fabrication.
The M30 fits lighter work, while M50 offers more margin for everyday sheet and medium-gauge parts. M70 is the stronger option when thicker stainless appears regularly.
Best for: General stainless fabrication where power and multi-process flexibility both matter.
Dynalasers D Series for Heavier Workshop Work
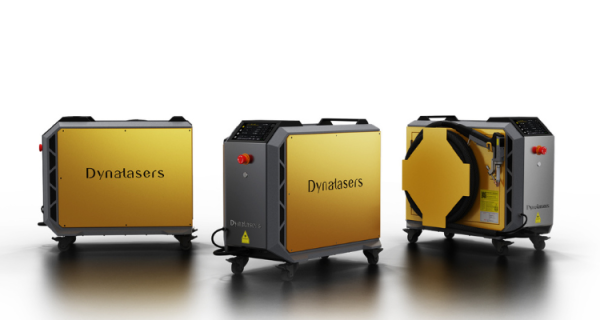
The D Series covers 1200W, 1500W, and 1800W and uses phase-change air cooling. D50, D60, and D70 support continuous, pulse, and spot welding, along with cleaning and light handheld cutting.
Published stainless-steel melting depths rise from about 5 mm on D50 to 6 mm on D60 and 7 mm on D70.
The D60 sits in a useful middle position for workshops that want 1500W capability without moving to a conventional water-cooled system. D70 gives more process margin for thicker parts and regular production.
Best for: Machinery repair, medium-thickness stainless, frames, fabricated assemblies, and busier multi-process workshops.
Dynalasers S Series for Thin Sheet and Mobile Jobs
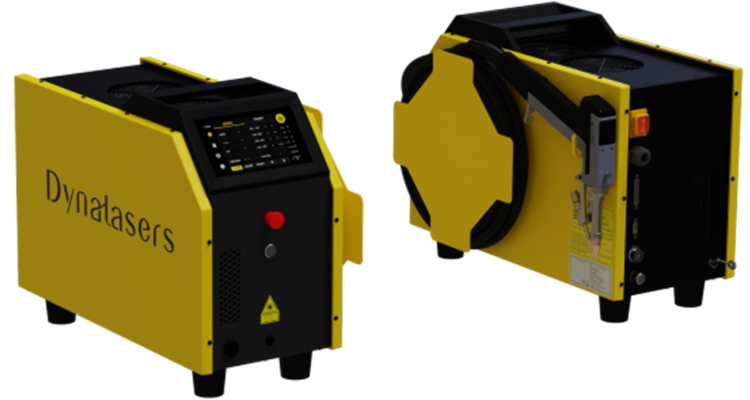
The S Series is built around portability rather than maximum depth.
The S30 produces 700W, weighs under 21 kg, measures roughly 507 × 230 × 349 mm, and uses a welding gun below 0.48 kg. Dynalasers publishes about 2.5 mm stainless-steel melting depth under its stated conditions.
That makes it more relevant to thin covers, cabinets, repair patches, short seams, and field maintenance than heavier fabrication.
When the workpiece is installed or difficult to move, bringing a compact machine to the part can matter more than adding another kilowatt of capacity.
Best for: Thin stainless sheet, compact shops, mobile maintenance, and on-site repair.
Laser Spot Welding Stainless Steel
Laser spot welding stainless steel deserves separate attention because not every joint needs a continuous seam.
Spot mode can be used for tacking, overlapping sheet, localized repair, or holding an assembly before a final weld. It can also reduce unnecessary heat when only specific joining points are required.
Dynalasers S10 supports spot welding alongside continuous and pulse operation, allowing the same machine to move between short localized joints and longer seams.
The joint still needs verification. A spot that looks secure may not provide enough fusion area for a loaded assembly.
FAQs
Can stainless steel be laser welded?
Yes. Stainless steel is widely suited to fiber laser welding, particularly for sheet metal, enclosures, cabinets, repair, and fabricated assemblies.
What are the downsides of laser welding stainless steel?
The process needs relatively consistent fit-up, clean joints, careful parameter control, and strict Class 4 laser safety.
How thick of stainless steel can a laser welder weld?
It depends on power and process conditions. Dynalasers publishes stainless melting depths from about 2.5 mm on S30 to around 7 mm on selected 1800W models.
What gas is best for laser welding stainless steel?
Argon is commonly used, but gas selection should match the stainless grade and welding procedure. Nitrogen can change weld metallurgy and should not be treated as interchangeable in every application.
Conclusion
Laser welding stainless steel is particularly effective when a shop wants fast seams, lower distortion, and less finishing on sheet-metal parts. The process still rewards good fit-up, clean surfaces, correct shielding, and verified penetration.
Dynalasers covers different workloads with three air-cooled ranges: S Series for mobile and thin-sheet work, M Series for everyday fabrication, and D Series for stronger regular production. The useful number on a specification sheet is not simply wattage. It is whether the machine can produce a stable, repeatable weld on the actual stainless part.


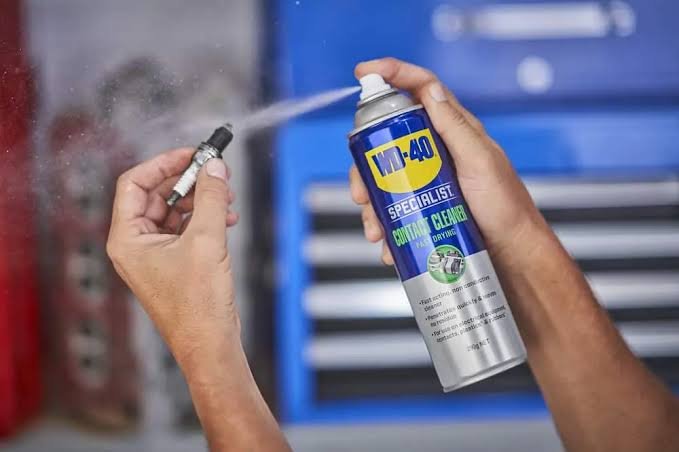
When dust, dirt, grease, and other contaminants are allowed to gather on electrical and electronic devices and equipment over time, this can adversely impact on their performance and reliability.
This helps draw attention to the usefulness of residue-free contact cleaners as a means of removing such deposits without leaving behind unwanted cleaning agents. These cleaners evaporate fast, help bring back conductivity, and help guard against intermittent faults or component failure.
It is also true, however, that contact cleaners aren’t all equally suitable for every application. This guide, then, will take a closer look at how residue-free formulations work, the components they can be used on, and the circumstances in which the use of residue-free contact cleaner tends to make most sense.
A Quick Introduction to Residue-Free Contact Cleaners
Residue-free contact cleaners are specialised solvent-based cleaning products designed to remove dirt, dust, and other contaminants from electrical contacts and electronic components without leaving any film, oily deposit, or sticky residue behind.
A key issue with some general-purpose degreasers or lubricants is that they may leave a protective film on the treated surface. This might not be desirable for certain applications, such as the cleaning of electrical contacts, given that such oily films or other residues may interfere with electrical conductivity, attract further dirt, or affect the operation of sensitive components.
Residue-free contact cleaners are typically non-conductive, offering high dielectric strength. Products in this category also tend to evaporate rapidly, in addition to being compatible with most plastics, rubber, metals, and coatings in modern equipment.
4 Circumstances in Which Residue-Free Contact Cleaners May Be Used
It is typically most appropriate to use residue-free contact cleaners whenever there is a need to clean electrical or electronic components without attracting new dirt, causing electrical shorts, or altering sensitive electrical signals.
This encompasses such applications and circumstances as:
- The Cleaning of Sensitive and Precision Electronics
Film left on the surface of an appliance or component after cleaning can act as an insulator or alter electrical resistance. As a result, data corruption or even device failure may occur.
On printed circuit boards (PCBs), for instance, a residue-free contact cleaner may be used to clear away dust, light oils, or leftover soldering flux without leaving a conductive path.
Such a cleaner can be greatly useful, too, for use on airflow meters, optical sensors, or medical equipment where even a microscopic film might skew readings.
- High-Dust or Industrial Environments
The wet and oily films that traditional sprays leave behind can behave like a magnet for airborne particles.
This is why residue-free cleaners are routinely used on control panels and switchgear, in acknowledgement of the sawdust, metal shavings, or concrete dust that can often be present across factories, workshops, or construction sites.
Power tools can also benefit from residue-free contact cleaners being used on them, given the triggers and battery terminal interfaces on such devices that are often exposed to outdoor dirt and grime.
- High-Voltage or Arc-Prone Components
The residue from standard cleaners can be highly flammable or carbonise in the event of an electrical arc. These can be major causes of concern when it comes to the cleaning of certain vulnerable components.
Relays and switches, for instance, are mechanical pieces that physically open and close, creating tiny sparks in the process. Depending on the specific product chosen, the use of a residue-free cleaner on these items can allow for the removal of oxidation and soot without potentially flammable oils being left behind.
However, it is critical to note that the exact electrical properties and flammability characteristics of contact cleaners vary, with some residue-free formulas being highly flammable. So, users must always check the manufacturer’s technical and safety instructions before use.
Circuit breakers and fuse blocks are further examples of components potentially well-suited to being cleaned with residue-free products. As far as this particular task is concerned, the maintenance of strict dielectric strength and the prevention of voltage leakage are critical priorities.
- Working Around Plastics and Rubber Housing
The tendency for many electrical contacts to be tightly encased in plastic bodies, or sealed with rubber gaskets, highlights another common application for residue-free cleaning products.
However, it is crucial to check first whether the can is explicitly labelled “plastic-safe” or “safe on rubber and plastics”. A contact cleaner being “residue-free” doesn’t automatically mean it won’t react with polymers; it simply means the liquid evaporates quickly without leaving an oily film.
Conclusion: In Certain Contexts, Residue-Free Options Can Be Indispensable
Residue-free contact cleaners can play a valuable role in the maintenance of electrical and electronic equipment. With no significant cleaning film being left behind, the user of residue-free cleaners can trust them to help deliver a clean and dry finish.
A cleaner that leaves no residue can be key to restoring conductivity while minimising the risk of future contamination buildup. Such a combination of qualities can go a long way to reducing the likelihood of recurring malfunctions, extending component life, and supporting the reliable operation of all manner of devices and systems.
Tech
Beyond the Homepage: How Web Development and Business Automation Build a Stronger Online Presence

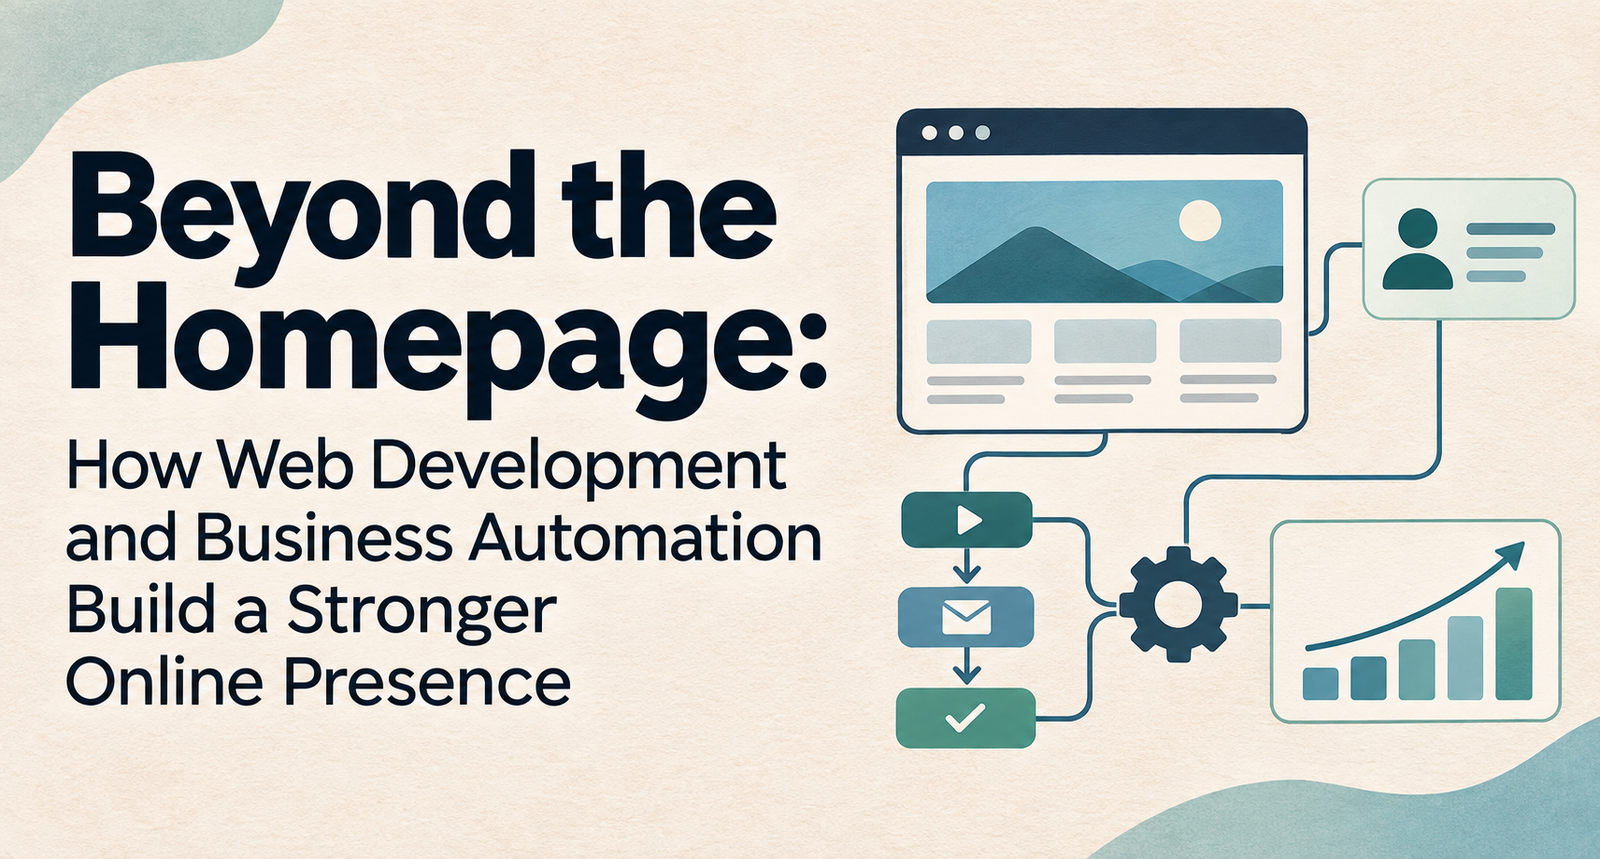
Most businesses judge their online presence by what they can see: the homepage design, the logo, the follower count. Customers judge it by what happens next. Does the page load on their phone in a busy parking lot? Can they find a price, book a slot, or get an answer at 9 p.m. on a Sunday? Or does their inquiry sit in an inbox until Tuesday?
That gap between first impression and follow-through is where many small and mid-sized businesses quietly lose customers. A strong online presence is really two things working together: a well-built website that earns attention and trust, and automated processes behind it that keep the promises the website makes.
This is why more owners are moving away from treating their site as a one-time design project. Working with a website development and digital marketing agency that looks at search visibility, site performance and lead handling as one connected job usually beats hiring separate vendors who never talk to each other.
The same thinking is spreading into industry-specific operations. A driving school, for example, can pair a fast, locally optimized website with driving school management software shaped around its own scheduling, instructor and student workflows. A parent who finds the school on Google can then book a lesson in minutes instead of waiting for a callback.
Below, we look at what each side contributes, where businesses commonly stumble, and a practical way to bring the two together.
Online Presence Is Now a Chain, Not a Page
A decade ago, being online mostly meant having a website. Today, a customer might first meet your business in a Google Maps listing, a review site, a social post, or an answer written by an AI assistant. Each of those touchpoints pulls information from somewhere, and much of it traces back to your website and the systems connected to it.
That makes your presence less like a storefront and more like a chain. Its links include:
- Discoverability: showing up in search results, map packs and AI-generated answers.
- Credibility: consistent business details, genuine reviews and clear service information.
- Responsiveness: how quickly someone gets a reply, a quote or a confirmation.
- Follow-through: reminders, updates and communication after the sale.
Good web development strengthens the first two links. Automation strengthens the last two. A weak link anywhere breaks the whole experience.
What Web Development Actually Contributes
Web development is often confused with web design. Design decides how a site looks. Development decides how it works, and that is what search engines, AI tools and impatient visitors notice first.
A few foundations matter more than any visual flourish.
Speed and mobile performance. Most local searches happen on phones. If a page drags, many visitors leave before they see your offer. Clean code, compressed images and reliable hosting do more for conversions than a clever animation.
Clear structure. Search engines and AI assistants reward sites that are easy to read. That means one clear topic per page, logical headings, descriptive page titles, and structured data, the behind-the-scenes labels that tell Google your hours, location and services.
Trust signals. Secure connections, working privacy policies, visible contact details and real customer stories reassure both people and algorithms that your business is legitimate.
Room to connect. This is the one owners overlook. A site built with forms, booking tools and integrations in mind can pass information straight into your other systems. A site that only displays brochure text becomes a dead end the moment a visitor wants to act.
The Moment After the Click
Plenty of businesses spend heavily to win a visitor’s attention, then hand that visitor to a manual process. A contact form lands in a shared inbox. Someone eventually copies the details into a spreadsheet, calls back, plays phone tag, and finally confirms by text.
Every step in that routine is a chance for the customer to go elsewhere. Business automation closes those gaps by letting routine work happen on its own:
- Inquiries get an instant, useful acknowledgment instead of silence.
- Bookings and payments happen in one sitting.
- Reminders go out without anyone having to remember them.
- Customer details flow into one record instead of five scattered files.
Automation is not about replacing people. It clears away the repetitive tasks that keep your team from the conversations that genuinely need a human, like a hesitant first-time buyer or an unhappy customer.
One Customer Journey, Two Systems Working Together
Picture a homeowner whose air conditioner fails on a hot July afternoon. Here is how a connected setup handles the next twenty minutes and beyond:
- They search for AC repair nearby and find a local HVAC company whose fast, mobile-friendly service page ranks well and answers common questions upfront.
- They tap “Book a visit,” choose a time slot pulled live from the technician calendar, and pay a small diagnostic fee.
- A confirmation arrives by text and email with the technician’s name and arrival window.
- On the morning of the visit, a reminder goes out. After the job, a short message asks for a review.
- That review appears on the company’s profile, strengthening its visibility for the next homeowner who searches.
Notice the loop. The website wins the visit, automation delivers the experience, and the experience feeds back into visibility. Neither half works nearly as well alone.
Where Businesses Commonly Get Stuck
If the combination works so well, why don’t more businesses have it? A few patterns come up again and again.
Tool sprawl. A booking app here, an email platform there, a payment processor somewhere else. Each solves a small problem, but together they create data islands and double entry. Map your customer journey first, then choose tools that connect, rather than adding apps one emergency at a time.
Off-the-shelf mismatch. Generic software often forces a business to bend its process around the tool. That is fine for standard tasks but frustrating for teams with unique workflows. In those cases, custom-built or highly configurable solutions usually pay off over time.
Automating a broken process. Software speeds up whatever you give it, including bad habits. Fix the workflow before you automate it.
Losing the human tone. Robotic messages feel cold. Write automated emails and texts the way your best employee would say them out loud.
This is where an experienced technology partner earns its keep. NewAgeSysIT, for example, builds custom software, mobile apps and AI-driven solutions for businesses, which gives it a practical view of how a public-facing website and internal operations should share data instead of living in separate worlds. The real value of a partner like that is seeing the full chain, not selling a single tool.
A Practical 90-Day Plan
You don’t need a full rebuild to get started. A phased approach keeps costs manageable and shows results early.
Days 1 to 30: Audit. Test your site on a phone, check page speed, and confirm your business name, address and phone number match everywhere online. Then list every manual step between a new inquiry and a completed sale.
Days 31 to 60: Fix the foundation. Tackle the biggest technical issues, sharpen your key service pages, and add a booking or quote form that feeds a calendar or CRM instead of an inbox.
Days 61 to 90: Automate the obvious. Set up instant inquiry replies, appointment reminders and review requests. Track response time and booking rate before and after, so you can see what actually changed.
Once these basics run smoothly, move on to deeper integrations such as online payments, customer portals or reporting dashboards.
Trends Shaping the Next Few Years
AI search is changing discovery. More people now ask AI assistants for recommendations. These tools favor businesses with clear, well-structured and consistent information, which makes solid development work more important than ever.
Customers expect self-service. Booking, rescheduling and paying without a phone call is fast becoming the norm rather than a perk.
Owned systems are gaining ground. Some businesses are rethinking stacks of monthly subscriptions and investing in platforms tailored to their workflow that they control for the long term.
Privacy expectations are rising. Collecting data responsibly, with clear policies and secure handling, is now part of earning trust online.
The Bottom Line
Your online presence is the sum of every interaction a customer has with you, not just the page they land on. Web development makes you easy to find and easy to trust. Automation makes you easy to do business with.
Start with the weakest link in your own chain, fix it, measure the difference, and build from there. The businesses that win online are rarely the flashiest. They are the ones that respond fastest and follow through every single time.

An AI PDF summarizer with flashcards and practice tests still has upload limits, so check them first. Adobe Acrobat’s flashcard maker accepts files up to 100MB and 600 pages, builds flashcards from key terms, definitions, and formulas, and links to quizzes, with no sign-up or credit card required to start.
Students who need to summarize long readings and turn them into study aids often hit a limit before they hit a result. Some limits count pages, some count megabytes, and some count words or sources. Knowing which one applies saves a failed upload and a lost evening. The sections below compare what several tools publish, using each tool’s own pages where possible, and explain how to plan around them. Limits change, so confirm them before you rely on one. Prices and caps change often, so check the tool’s own page.
File Upload Size Limit for a PDF: What Do Tools Allow?
It varies, and the unit differs. Adobe Acrobat’s flashcard maker accepts files that are 100MB or smaller and 600 pages or fewer, tells users to upload a smaller PDF when a file is too large, and limits prompts to 1,000 characters. Its page also lists errors for empty files and unsupported formats, so check that the file opens normally first. Its Student Spaces page also includes an AI Assistant for chatting through course material. Gemini Notebook, formerly NotebookLM, allows each source up to 500,000 words or 200MB for uploaded files, with up to 50 sources on the free plan, and Google’s help page says it offers two modes for summarizing sources. Quizlet says you can paste up to 100,000 characters in one session. The table compares the published limits. Split a very long PDF by chapter before uploading, and keep a copy of the original. If you only need a short section, copy the key pages into a new file so the AI has less to read and you stay far below any cap.
| Tool | Published limit | Count | Outputs |
| Adobe Acrobat flashcard maker | 100MB and 600 pages per file; prompts up to 1,000 characters | Per file | Flashcards; links to quizzes, study guides, mind maps, AI Assistant |
| Gemini Notebook | 500,000 words or 200MB per source; 50 sources on the free plan | Per source | Summaries, flashcards, quizzes, study guides |
| Quizlet | 100,000 characters of pasted text per session | Per session | Study guides, flashcards, quizzes |
Source Limit: How Do 200 MB and 500,000 Words Work Together?
Gemini Notebook’s help page lists both numbers for each source: up to 500,000 words or up to 200MB for uploaded files, so whichever you reach first is the real limit. A scanned PDF full of images tends to reach the megabyte cap first, while a text-heavy file reaches the word cap first. Free users can include up to 50 sources, and inactive sources still count toward the limit, so remove ones you no longer need. The help page also says PDFs added through URLs are treated as PDF sources. For planning, assume a page holds about 500 words, which makes 500,000 words roughly a thousand pages, an estimate that varies with formatting. Check the word count in a document editor if you are unsure. Most course readings fit easily, but a full textbook with figures may not. Ask for a summary of one section first, then check how well it matches before you commit a whole book.
Frequently Asked Questions
How should I summarize a very long PDF?
Work in stages. Summarize one chapter at a time, check each summary against the page it came from, and then combine the chapter summaries into a study guide or flashcard set. Tools that offer more than one summary mode, such as Gemini Notebook, let you pick a shorter or longer version. Keep your own notes for anything the summary misses. Save each chapter summary in one document so you can review them in order. Rewrite any sentence you do not understand.
Can I make flashcards and practice tests from the same PDF?
Often. Adobe Acrobat’s page links to quizzes, study guides, and mind maps built from your materials, Gemini Notebook generates flashcards and quizzes from uploaded sources, and Quizlet says one upload can produce a study guide, flashcards, and quizzes. Use the flashcards to learn terms and the practice tests after a gap to check recall. Keep one set per chapter so tests stay focused. Mix question types if the tool offers them. Retry missed items on a later day.
What if my PDF is over the limit?
Reduce it. Split the file by chapter, remove blank pages and long reference lists, and upload the sections you need. If a file is large because of images, export a text-focused version when your course allows it. Adobe Acrobat’s page suggests uploading a smaller PDF, and Google’s limits count both words and megabytes. Tell the tool which pages matter so it does not spend effort on appendices. Check the result against the page before you study from it.

How to Get the Most Out of a London Event Venue Site Visit

How to get a better shower without a full bathroom renovation

Why Trying On Engagement Rings Can Change Your Shortlist

Extend or Move? Why More Londoners Are Building Instead of Buying

Lab-Grown vs Natural Diamonds: How to Choose an Engagement Ring

The Latest Women’s Fashion Trends to Shop at SHEIN

How to Ensure Your Home is Valued Correctly for a Quick Sale
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon

The 15 Highest-Paid Rugby Players in the World

What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement

Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats

Who Is Azriel Crews? Inside the Life and Career of Terry Crews’ Daughter
How to Ensure Your Home is Valued Correctly for a Quick Sale
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon
The 15 Highest-Paid Rugby Players in the World
What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement
Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats
Who Is Azriel Crews? Inside the Life and Career of Terry Crews’ Daughter
-
 Real Estate10 months ago
How to Ensure Your Home is Valued Correctly for a Quick Sale
-
Celebrity12 months ago
Christopher Dare: The Untold Story of Engineer and Former Husband of Angela Rippon
-
 Sports6 months ago
The 15 Highest-Paid Rugby Players in the World
-
 Technology6 months ago
What Is Fanquer? The Digital Creator Platform Transforming Direct-to-Fan Engagement
-
 Celebrity6 months ago
Dr Jared Ross: Missouri Appeals Court Upholds Protection Order Over Graphic Torture and Murder Threats
-
 Celebrity9 months ago
Who Is Azriel Crews? Inside the Life and Career of Terry Crews’ Daughter
-
 Celebrity1 year ago
Nancy Hallam: The Inspiring Life, Career, and Success Story Behind Ian Wright’s Wife
-
 Celebrity1 year ago
Who Is Maisie Mae Roffey? The Private Life, Family Story, and Quiet Success of Julie Walters’ Daughter